Precision-engineered, audit-ready wholesale formulations manufactured under Canadian GMP, Health Canada, and US FDA compliant facilities for global market delivery.
Operating out of Canadian headquarters with global GMP-certified production facilities, we deliver absolute compliance, scientific formulation depth, and seamless global export logistics.
Our global manufacturing footprint is strictly compliant with Health Canada Site Licences, US FDA 21 CFR Part 111 cGMP standards, ISO 22000, and HACCP guidelines, ensuring smooth customs release across North America, Europe, and the GCC region.
Every raw lot and finished batch undergoes rigorous HPLC potency testing, ICP-MS heavy metal screening (Lead, Arsenic, Cadmium, Mercury), and complete microbiological validation, supported by ISO 17025 third-party certificate verification.
Overcome the natural chalkiness, astringency, and earthy off-notes of botanical proteins. Our in-house flavor technologists utilize microencapsulation, natural masking agents, and micronization for supreme mixability and velvety mouthfeel.
The global transition toward plant-based nutrition has evolved from a niche lifestyle demand into a primary driver of the global food and nutraceutical processing economy. Brand owners, clinical formulation teams, and retail distributors seeking to capture market share must navigate complex biochemical challenges: achieving complete essential amino acid (EAA) profiles, maximizing protein digestibility-corrected amino acid scores (PDCAAS), optimizing organoleptic profiles without artificial additives, and guaranteeing allergen-segregated processing integrity.
As a senior B2B contract development and manufacturing organization (CDMO), our plant protein manufacturing protocols integrate modern food science with strict regulatory oversight. This technical guide outlines the critical parameters required to specify, engineer, and commercialize market-leading plant protein formulas.
A central challenge in plant protein formulation is that single botanical sources frequently exhibit limiting amino acids. For instance, yellow pea protein isolate (Pisum sativum) is rich in lysine and branched-chain amino acids (BCAAs) such as leucine, isoleucine, and valine, but naturally low in sulfur-containing amino acids methionine and cysteine. Conversely, brown rice protein isolate (Oryza sativa) contains high levels of methionine and cysteine but lacks sufficient lysine.
By engineering a precise **70:30 Pea-to-Rice Protein Isolate Matrix**, our formulation team constructs a complementary amino acid architecture that achieves a **PDCAAS score of 1.0**—equating to the biological efficacy of premium whey or egg albumin. Additionally, we provide custom integration of pumpkin seed, sacha inchi, sunflower, and fava bean proteins to enhance micronutrient density (magnesium, zinc, iron) and tailor kinetic release rates.
| Protein Isolate Base | Protein Concentration (%) | Limiting Amino Acid | Key Strengths | Recommended Application |
|---|---|---|---|---|
| Yellow Pea Protein Isolate | 80% – 85% | Methionine / Cysteine | High Lysine, BCAA rich, hypoallergenic, non-GMO | Sports nutrition, mass gainers, meal replacements |
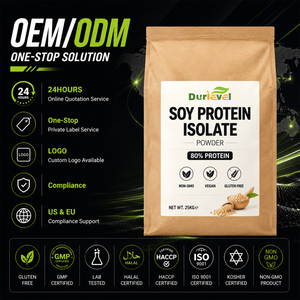
| Soy Protein Isolate (SPI) | 90% Min | Methionine (slight) | Complete protein, superior emulsification & gelation | Clinical nutrition, meat analogs, beverage bases |
| Enzymatic Brown Rice Protein | 80% – 90% | Lysine | High Methionine, smooth texture, low allergenicity | Synergistic pea blends, clean-label organic powders |
| Fava Bean / Pumpkin Seed Blend | 65% – 75% | Threonine | Neutral flavor, rich in natural minerals, high solubility | Functional RTD beverages, bakery fortification |
Commercial viability in the retail segment is overwhelmingly determined by flavor acceptance and digestive tolerance. Raw botanical extracts naturally contain polyphenols, hexanal compounds, saponins, and phytic acid—substances responsible for bitterness, astringency, off-gassing, and mineral chelation.
To further elevate product differentiation, modern OEM/ODM plant protein formulations incorporate bio-active digestive matrices. Plant proteins generally exhibit a slower gastric digestion rate compared to hydrolysed animal proteins. To solve this, we offer turn-key blending of endogenous fungal enzymes including Aspergillus niger derived proteases, papain, bromelain, and α-galactosidase—specifically targeted to hydrolyze complex oligosaccharides (raffinose, stachyose) responsible for gastrointestinal discomfort.
Furthermore, integrating prebiotic soluble fibers such as organic agavin, acacia gum, and resistant dextrin creates a dual-action formula supporting gut microbiota proliferation while providing a creamy viscosity profile without relying on synthetic gums (CMC or xanthan).
Key technological, regulatory, and consumer shifts transforming B2B sourcing strategies for brand owners over the next decade.
The next frontier merges traditional botanical isolates (pea, soy) with precision-fermented bio-identical proteins and microalgae (chlorella, spirulina). OEM brands are adopting these hybrid systems to achieve unprecedented amino acid density and animal-free dairy identical functionality.
Enterprise buyers and retail chains now mandate Scope 1-3 carbon footprint disclosure. Sustainable sourcing models focusing on dry-fractionation processing—which uses 90% less water and energy than traditional wet chemical extraction—are rapidly becoming prerequisite criteria for export contracts.
With tightening international regulations (California Proposition 65, EU Heavy Metal Regulations), brands require certified raw material provenance. Sourcing pea and rice crops from validated, low-heavy-metal soils with lot-level ICP-MS documentation is now essential for legal security.
Practical operational clarity sourced directly from our contract manufacturing, regulatory affairs, and logistics engineering teams.
Our standard manufacturing MOQs are structured to accommodate both scaling DTC brands and high-volume retail distributors: 500 kg for custom powder blending runs, 1,000 units for stock private-label retail tubs (700g/907g), and 25kg Kraft bags for raw ingredient bulk supply. Pilot validation batches for stability and consumer testing can be arranged under specific CDMO agreements.
Production facilities enforce rigorous allergen control programs (ACP) in full alignment with cGMP and ISO 22000 mandates. Operations utilize physically segregated processing suites, dedicated pneumatic conveying lines, and validated ELISA swab cleaning protocols between production cycles to guarantee zero cross-contamination for allergen-free (soy-free, gluten-free, dairy-free) product claims.
Every commercial shipment is accompanied by a full technical dossier including: Batch Certificate of Analysis (COA), Certificate of Free Sale (CFS), Health Canada / FDA Compliance Attestation, Allergen Statement, Non-GMO Declaration, BSE/TSE Free Certificate, Heavy Metal Test Summary, and Country of Origin Certification. Our regulatory team handles local NPN submissions and EU food supplement notification dossiers upon request.
For stock private-label formulations with standard packaging, typical lead times range from 4 to 6 weeks. Fully custom R&D projects—encompassing flavor profiling, pilot blending, accelerated stability testing (40°C / 75% RH), and custom printed film or tub procurement—are delivered within 8 to 12 weeks from specification approval.
From primary barrier packaging selection to DDP door-to-door freight forwarding, we safeguard product shelf-life and supply chain continuity.
Multi-wall 25kg food-grade Kraft paper bags with heat-sealed PE inner liners. Ideal for industrial food processors, secondary packagers, and institutional supply.
100% recyclable, UV-shielded plastic tubs (450g to 2.5kg) featuring induction-sealed tamper-evident liners and custom debossed dosing scoops.
High-barrier aluminum foil laminate sachets (15g–35g) engineered for zero moisture vapor transmission (MVTR), providing convenient on-the-go dosing.
Resealable press-to-close zipper pouches with matte/gloss spot finish, metallic foil barriers, and high-impact shelf presentation for DTC brands.
Accelerate your product launch with our certified CDMO infrastructure, scientific R&D team, and international export expertise. Request custom quotes, product samples, or factory audit schedules today.
Contact Us