
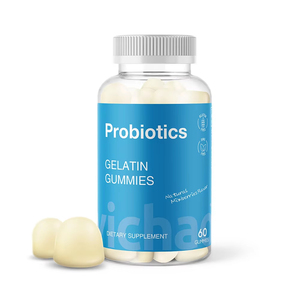
S-Probiotics Pectin Gummy Gut Health Vitamin Gummy Candy Bacillus Coagulans
Pack Spec: Active Desiccant HDPE Bottle | Moisture Lock Cap
Get Catalog
Featured OEM/ODM packaging configurations optimized for barrier protection, shelf-life stability, and shelf impact across global markets.
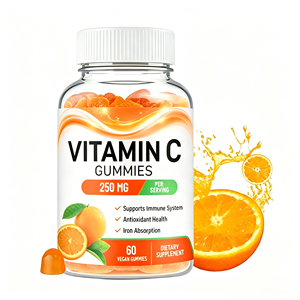
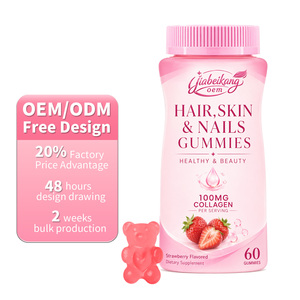
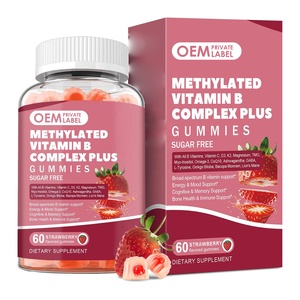
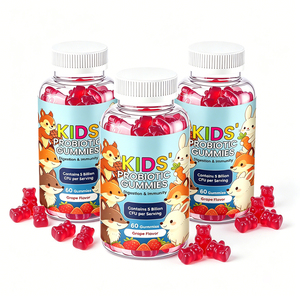
In the modern global health, pharmaceutical, and nutraceutical sectors, rigid bottle packaging has evolved far beyond passive containment. Today’s brand owners, contract manufacturers, and procurement directors recognize that container integrity directly dictates chemical stability, active constituent potency retention, shelf-life validation, and regulatory compliance. Selecting an OEM/ODM bottle manufacturing partner requires a precise balance of polymer material science, barrier engineering, closure mechanics, and high-speed automated packaging synchronization.
Protecting active ingredients (such as live probiotics, delicate omega fatty acids, and hygroscopic botanical extracts) against oxygen ingress, relative humidity, and ultraviolet photodegradation through optimized polymer formulations.
Fully automated bottling integration utilizing multi-head electronic tablet/gummy counters, automated desiccant packet/canister insertion, induction heat sealers, and vision-guided label applicators running at up to 150 BPM.
Manufacturing containers under stringent cGMP, Health Canada NHP, and US FDA 21 CFR Part 111/211 standards, backed by full extractable and leachable (E&L) testing documentation and heavy metal purity verification.
A rigorous comparison of primary bottle packaging materials used across dietary supplement, pharmaceutical, and functional food manufacturing.
| Polymer / Material | Moisture Barrier (MVTR) | Oxygen Barrier (OTR) | UV Light Protection | Impact Resistance | Sustainability / Recyclability | Primary Application |
|---|---|---|---|---|---|---|
| HDPE (High-Density Polyethylene) | Superior (< 0.05 g/100in²/day) | Moderate | Excellent (Opaque / White) | Very High | 100% Recyclable (RIC #2) | Hygroscopic powders, chewables, probiotics, tablets |
| PET (Polyethylene Terephthalate) | Good | Excellent (< 0.1 cc/100in²/day) | High (Amber / Cobalt Tint) | High (Shatterproof) | 100% Recyclable (RIC #1) | Gummy vitamins, softgels, clear cosmetic liquids |
| rPET / PCR-PET (Post-Consumer Recycled) | Good | Good to Excellent | Custom Tint Available | High | Closed-Loop Eco Standard | Eco-conscious DTC brand lines, sustainable retail SKUs |
| Amber Glass (Type III Pharmaceutical) | Absolute Zero Permeability | Absolute Zero Permeability | Maximum UV Shield (< 450nm) | Low (Fragile) | Infinitely Recyclable | Clinical formulations, botanical tinctures, oxidation-sensitive oils |
| Aluminum (Seamless Rigid Containers) | Absolute Zero Permeability | Absolute Zero Permeability | 100% Light Proof | Extreme | High Value Recycling | Premium sports nutrition, RTD shots, eco-luxe supplements |
From custom CAD container geometry to final bonded warehouse dispatch, our 6-stage engineering protocol minimizes time-to-market while safeguarding product stability.
Custom container shape engineering, volumetric capacity calculations, neck finish sizing (e.g., 38-400, 45-400), and rapid 3D printing of ergonomic samples for hands-on brand approval.
Fabrication of hardened steel or aircraft-grade aluminum blow-molding and injection-molding cavities designed for high-tonnage, multi-cavity high-speed production runs.
Automated Injection Stretch Blow Molding (ISBM) and Extrusion Blow Molding (EBM) executing uniform wall thickness, crystal-clear optical clarity, or zero-light opacity.
Cleanroom filling equipped with multi-channel optical sensor tablet counters, desiccants/oxygen absorber insertion, and nitrogen gas flushing for oxidation protection.
Application of hermetic induction foil heat seals, child-resistant push-and-turn closures, and vision system confirmation of cap torque specifications (in-lb tolerance testing).
High-precision pressure-sensitive or shrink-sleeve labeling, inkjet batch/EXP coding, 2D matrix serialization, and heavy-duty corrugated master cartoning for export shipping.
The global contract packaging landscape is undergoing structural shifts driven by regulatory tightening (such as extended producer responsibility laws and single-use plastic mandates), consumer demand for eco-transparency, and the rise of high-efficacy active nutraceutical formulations. Procurement leaders must align with OEMs capable of navigating these four critical trends:
Brands are shifting from virgin resins to 30%, 50%, and 100% Post-Consumer Recycled (PCR) PET and HDPE bottles. Modern OEM factories must utilize advanced decontamination and resin-blending techniques to maintain mechanical strength, wall integrity, and food-contact FDA food-grade compliance without yellowing or structural micro-cracks.
Conventional loose desiccant packets are increasingly replaced by molecular sieve integrated cap liners and active desiccant-entrained polymers molded directly into bottle walls. This eliminates ingestible desiccant risk while maintaining sub-10% internal humidity levels for sensitive probiotic, enzyme, and moisture-labile formulations.
Global regulations (ISO 8317 and US 16 CFR § 1700.20) require child-resistant (CR) packaging that remains senior-friendly (SF). Next-generation squeeze-and-turn and push-and-turn closures utilize tactile grip ridges and low-torque release mechanics to balance child safety with accessibility for elderly consumers.
With cross-border e-commerce expanding globally, illicit supplement diversion and brand counterfeiting present major commercial risks. Advanced OEM bottling lines now integrate high-resolution UV micro-printing, unique 2D DataMatrix QR codes, and tamper-evident neck shrink sleeves to enable real-time supply chain authentication and track-and-trace monitoring.
As a Health Canada Licensed, US FDA Registered, and cGMP Certified Contract Development and Manufacturing Organization (CDMO) headquartered in Mississauga, Ontario, Q Nutritions bridges technical formulation expertise with advanced bottle packaging engineering. Our dual North American regulatory footprint and audited global factory footprint allow brand owners to scale seamlessly from 1,000-unit market pilot runs to multi-container commercial distributions.
In-depth responses from our senior packaging engineers and regulatory specialists.
Our minimum order quantities start at 1,000 to 5,000 units for standard stock bottle configurations (HDPE, PET) with custom private label artwork and induction sealing. For fully customized container geometries requiring custom injection/blow molds, MOQs typically begin at 10,000 to 25,000 units depending on cavity size and resin formulation. Pilot testing batches are available for stability testing and regulatory filing validation.
Every bottle material and closure combination undergoes rigorous Moisture Vapor Transmission Rate (MVTR) testing according to USP <671> protocols. We utilize high-density opaque HDPE or specialized amber PET bottles equipped with active silica gel or molecular sieve desiccant liners. In-line automated induction heat sealing creates a hermetic seal, verified by vacuum decay leak testing and continuous relative humidity monitoring during accelerated stability studies (40°C / 75% RH).
For stock bottle formats with standard closures, typical production turnarounds range from 4 to 6 weeks from final artwork sign-off. For custom OEM bottle shapes requiring 3D CAD modeling, steel mold tooling fabrication, sampling, and pilot testing, total lead times are generally 8 to 12 weeks. We maintain extensive stock inventory of standard 60cc, 100cc, 150cc, 200cc, and 250cc bottles to support rapid product launches.
Yes. All our child-resistant (CR) closures comply fully with US 16 CFR § 1700.20 standards and ISO 8317 international protocols. We offer multiple ergonomic designs including push-and-turn, squeeze-and-turn, and snap-double-push closures. Full protocol testing reports from third-party certified testing facilities are provided for regulatory submission in North America, Europe, Australia, and the GCC region.
Our in-house Regulatory Affairs and Package Engineering teams provide complete label compliance screening across Health Canada Natural Health Product (NHP) regulations, US FDA Supplement Facts formatting, European Union Food Supplement Directives, and GCC food safety standards. We ensure correct font sizing, allergen declarations, net content formatting, and metric/imperial conversions before printing.
We supply food-grade 100% Post-Consumer Recycled PET (rPET), PCR-HDPE, and plant-based Bio-PE bottles derived from sugarcane waste. Additionally, we engineer lightweighted bottles that reduce total resin usage by up to 25% without sacrificing top-load compression strength or seal integrity during transit.
All contract bottling takes place inside positive-pressure ISO Class 8 (Class 100,000) cleanrooms operating under strict cGMP protocols. Bottling lines feature dedicated contact tooling, HEPA air filtration, automatic dust extraction, and validated clean-in-place (CIP) and swab verification procedures between product allergen runs (e.g., dairy-free, gluten-free, soy-free lines).
Every commercial delivery includes a comprehensive documentation binder containing: Batch Production Records (BPR), Certificate of Analysis (COA) for active finished goods, Certificate of Conformance (COC) for bottle/cap materials, Heavy Metal Purity Reports (ICP-MS), Microbiological Screening Results, and Free Sale Certificates (FSC) for export customs clearance.
Whether you require custom CAD container engineering, rapid prototyping, high-barrier probiotic packaging, or high-speed contract filling, our engineering team is ready to review your specifications.