The Dynamics of High-Compliance Contract Packaging in China
Navigating the global nutraceutical market requires contract packaging manufacturers that seamlessly integrate international pharmaceutical standards, advanced materials science, and cost-effective high-volume output. As a premier China Best Contract Packaging Manufacturer & Exporter, our operational framework bridges the gap between raw ingredient processing and fully compliant consumer packaging. Operating under dual North American and Asian manufacturing footprints, we empower global supplement brands, pharmaceutical distributors, and direct-to-consumer platforms to scale their supply chains securely.
Modern contract packaging extends far beyond simple bottle-filling or sachet sealing. It is a critical node in maintaining bio-activeness, ensuring shelf-life stability, preventing cross-contamination, and securing cross-border regulatory acceptance. Our facilities maintain strict alignment with US FDA 21 CFR Part 111 regulations, Health Canada Site Licences, and European Commission food supplement directives (EC 2002/46). By implementing real-time analytical verification and fully automated packaging lines, we mitigate the risk of degradation for delicate compounds such as spore-forming probiotics (Bacillus coagulans), heat-sensitive methylated B-vitamins, and lipid-soluble antioxidants.
Information Gain Insight: Advanced primary packaging selection directly influences active component decay curves. For instance, transitioning unstable probiotic formulations from standard PET bottles to high-barrier cold-form aluminium blister cavities or desiccant-lined HDPE bottles reduces water vapor transmission rates (WVTR) to near zero (<0.01 g/m²/24h), extending viable CFU counts by up to 300% across a standard 24-month shelf life.
Full Regulatory Traceability
End-to-end electronic batch records (EBR), lot-level genealogy, and independent third-party lab confirmation (HPLC, ICP-MS) supplied with every production run.
Multi-Dosage Capability
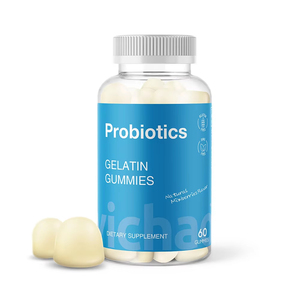
Engineered packaging setups for pectin/gelatin gummies, hard-shell vegan HPMC capsules, compressed tablets, softgels, and microencapsulated powders.
Scalable Procurement MOQs
Pilot runs starting at 1,000 units for encapsulated lines up to full container-load (FCL) continuous automated gummy bottling lines.
Enterprise Advantage: Integrated Global Manufacturing Network
Our manufacturing matrix blends strategic sourcing across North America, China, India, and the UAE to deliver unmatched supply chain resiliency. By maintaining state-of-the-art packaging facilities equipped with ISO Class 7 and Class 8 cleanrooms, we eliminate airborne particulates, humidity spikes, and microbiological contamination during primary encapsulation and filling cycles.
Whether client requirements demand private label turn-key solutions or custom formulation development, our in-house team of analytical chemists, regulatory specialists, and mechanical packaging engineers provide end-to-end guidance. We oversee the entire transformation pathway: from raw botanical extraction and active assay quantification to protective barrier selection, automated cartoning, and international customs clearance.
Packaging Format
Barrier Efficiency Level
Optimal Active Ingredients
Target Regulatory Certificate
Alu-Alu Cold Form Blister
Maximum (WVTR <0.005 g/m²/day)
Probiotics, Hygroscopic Extracts, B-Complex
US FDA, Health Canada NPN, EU GMP
Desiccant HDPE Bottling
High (Moisture & Light Shielded)
Pectin Gummies, Softgels, Multivitamins
GMP, ISO 22000, HACCP
Stick Pack Nitrogen-Flushed
High (Zero Oxygen Headspace)
Super Greens Powders, Collagen Peptides
Halal, Kosher, Organic USDA
Blister Thermoformed PVC/PVDC
Moderate to High Barrier
Minerals, Vitamin C, Effervescent Tablets
ISO 9001, NSF Certified
Strategic Procurement & Packaging Trends in 2026 and Beyond
As global demand for functional wellness products escalates, contract packaging must evolve to meet stringent sustainability mandates and changing consumer consumption habits. Global buyers are transitioning away from heavy glass containers and non-recyclable multi-layer plastics toward mono-material eco-polymers, post-consumer recycled (PCR) resin bottles, and biodegradable barrier films without sacrificing active constituent integrity.
Furthermore, precision dosing and micro-format packaging are accelerating across major markets. Consumers increasingly demand unit-dose sachets, stick packs, and blister packs that accommodate on-the-go lifestyle needs while safeguarding formulations against thermal degradation and ambient oxidation. Contract packaging partners must therefore possess dual capabilities: maintaining high-speed automated output while offering granular customizability for niche product lines such as methylated B-vitamin matrices (with TMG and Ashwagandha) or sugar-free pectin functional bear gummies.
Sustainable PCR Materials
Full integration of food-grade PCR-PET and rHDPE resins reducing carbon footprint while maintaining strict FDA food contact safety compliance.
Active Moisture Management
In-cap desiccant integration and oxygen absorber dosing inside bottling lines to stabilize moisture-sensitive active botanicals.
Anti-Counterfeit Serialisation
Implementation of 2D DataMatrix barcode printing and tamper-evident induction seals for brand security across export channels.
The contract manufacturing ecosystem is undergoing a fundamental shift toward smart automation, artificial intelligence quality inspection, and specialized bio-delivery formats. Industry leaders are focusing investments on high-gain manufacturing technologies that directly improve consumer efficacy and compliance:
Spore-Forming Probiotic Microencapsulation: Traditional live strain probiotics suffer severe attrition during thermal gummy processing. Next-generation contract packaging utilizes spore-forming strains like Bacillus coagulans coupled with protective lipid coatings, guaranteeing shelf stability without cold-chain storage.
Smart Packaging & RFID Supply Chain Tracking: Integrating ultra-thin RFID tags directly into primary carton packaging enables continuous temperature monitoring and real-time inventory management across transoceanic shipping routes.
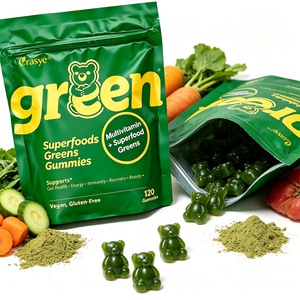
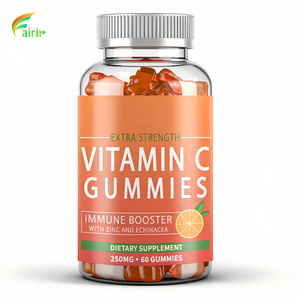
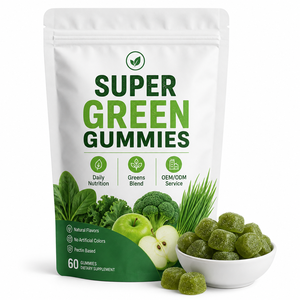
Sugar-Free Pectin Matrix Gelation: With global health metrics prioritizing sugar reduction, our R&D teams have perfected heat-stable, sugar-free pectin gelation matrices that accommodate high active loads (such as Vitamin C, Collagen, or Super Greens) without textural weeping or degradation over time.
Comprehensive B2B Procurement FAQ
What are your baseline Minimum Order Quantities (MOQs) for custom packaging projects?
Our MOQs are structured to accommodate both emerging brand pilots and high-volume commercial scaling. Standard encapsulated products (capsules, softgels, tablets) start at 1,000 unit bottles or 50,000 loose units. Custom gummy manufacturing starts at 5,000 retail bottles or 500 kg for bulk powder blending runs. Pilot batches are available for stability testing and regulatory registration submissions.
How do you verify active ingredient potency and finished product purity?
Every raw material lot undergoes analytical identity testing via High-Performance Liquid Chromatography (HPLC) or Fourier-Transform Infrared Spectroscopy (FTIR) upon arrival. Finished goods undergo rigorous testing for potency, heavy metals (ICP-MS), microbial contaminants (USP <2021/2022>), and residual solvents. A comprehensive Certificate of Analysis (COA) is issued for every production batch.
What international regulatory support do you provide for export products?
Our dedicated regulatory affairs division prepares full documentation dossiers required for cross-border clearance. This includes Health Canada Natural Product Number (NPN) applications, US FDA Supplement Facts panel compliance checks, EU food supplement notifications, GCC registration files, Certificates of Free Sale (CFS), and Certificates of Origin (COO).
Can you formulate sugar-free, vegan, and allergen-segregated delivery formats?
Yes. We operate dedicated allergen-controlled manufacturing lines equipped with validated CIP (Clean-in-Place) protocols. We specialize in 100% plant-based HPMC vegan capsules, citrus pectin-based gummies, organic-certified powder blends, and sugar-free formulations utilizing natural stevia or erythritol sweeteners.
What are the typical project turn-around lead times from formulation to final shipment?
Standard private-label packaging using pre-validated stock formulas typically ships within 6 to 8 weeks from artwork sign-off. Fully custom formulations requiring R&D trials, flavor matching, active stability testing, and custom primary packaging tooling generally require 8 to 12 weeks from specification approval.
Partner With China's Leading Contract Packaging Exporter
Consult with our engineering team today to review your formulation requirements, request custom quotes, or schedule a virtual site audit of our GMP-certified packaging facility.