High-potency, bioavailable, and stability-tested soft capsule formats manufactured under cleanroom conditions with full analytical validation.
An authoritative analysis of lipophilic dosage form engineering, global market access criteria, and OEM/ODM contract manufacturing standards.
Executive Summary: Modern nutraceutical branding requires pharmaceutical-grade precision. As a premier CE certified bulk softgels manufacturer and OEM/ODM factory, our facility integrates high-precision rotary die encapsulation technology, nitrogen-purged processing environments, and rigorous analytical testing to guarantee active ingredient protection, zero cross-contamination, and extended shelf stability for international distribution.
The global market for lipophilic dietary supplements is undergoing a massive paradigm shift. Buyers across the European Union, North America, and Asia-Pacific are moving beyond generic oil fills toward complex active delivery systems. Procurement teams prioritizing supply chain security must adapt to three key trends:
Technological advancement in softgel encapsulation machinery allows contract manufacturers to process challenging ingredients that were previously unstable in oil matrices. Key technical capabilities driving market innovation include:
Compare our pharmaceutical-grade contract manufacturing benchmarks against industry standard baseline specifications.
| Quality Parameter | Standard Industry Baseline | Our Factory Cleanroom Standard | Analytical Verification Method |
|---|---|---|---|
| Encapsulation Precision | ± 5.0% Fill Weight Variance | ± 1.5% Fill Weight Precision | Automated Micro-Balance Sampling (Statistical Process Control) |
| Dissolution Time | Under 45 Minutes (Gelatin) | Under 15 Minutes (Fast-Disintegrating Shell) | USP <701> Disintegration Apparatus |
| Peroxide Value (PV) | < 5.0 meq/kg (Oils) | < 1.5 meq/kg (Ultra-Pure Lipid Shield) | AOCS Cd 8b-90 / Potentiometric Titration |
| Heavy Metals (Pb, Cd, Hg, As) | < 10.0 ppm Combined | < 0.1 ppm Individual (Ultra-Trace Clean) | ICP-MS (Inductively Coupled Plasma Mass Spectrometry) |
| Microbiological Baseline | Total Plate Count < 1,000 CFU/g | Total Plate Count < 100 CFU/g (Pathogen Free) | USP <2021> / <2022> Automated Plating & PCR screening |
| Shell Elasticity & Leakage | Standard Visual Inspection | 100% Automated Vacuum Leak Detection | High-Pressure Vacuum Seal Testing Chamber |
From turnkey private label development to complex custom formulations, our plant operates as a dedicated CDMO center of excellence.
Our production ecosystem strictly adheres to EU CE directives, Health Canada Site Licences, US FDA Facility Registrations, ISO 22000, and HACCP standards. Complete regulatory dossiers—including Free Sale Certificates (FSC), Certificates of Origin (COO), and BSE/TSE-Free attestations—are generated directly by our in-house compliance team.
Equipped with over 15 automated high-speed softgel encapsulation lines capable of outputting over 3.5 billion capsules annually. We accommodate diverse shapes and sizes—including Oval (3, 7.5, 10, 20), Oblong (5, 10, 20, 1400mg), Round, and Custom Tube/Dropper formats with laser etching options.
Full-service packaging flexibility designed for freight protection and direct retail placement. Choose from high-density polyethylene (HDPE) bottles, amber glass jars, blister packaging (Alu-Alu & PVC/PVDC), shelf-ready display boxes, or bulk foil-lined drum containers for localized secondary filling.
In-house formulation scientists specializing in lipid-soluble ingredient stabilization, botanical extract blending, and organoleptic enhancement. We optimize capsule scent, shell clarity, opacity, and natural flavor masking (sweet orange, vanilla, peppermint) to boost consumer compliance.
Every production batch undergoes raw material identity confirmation (FTIR/NIR), in-process seal-width optical monitoring, and finished product potency testing (HPLC). Certificate of Analysis (COA) records are issued for every lot, supported by retained sample storage for full shelf-life traceability.
With extensive experience exporting to over 40 countries, our logistics team manages customs clearing documentation, temperature-controlled container shipments, and flexible Incoterms (FOB, CIF, DDP) to ensure zero thermal degradation during transit.
Discover how our OEM/ODM custom development capabilities power top-selling dietary supplement categories globally.
Oral nutricosmetics represent one of the fastest-growing dietary supplement sectors worldwide. Formulating active skin-brightening and anti-aging agents into softgels provides superior bio-protection compared to traditional dry tablets.
Technical Advantage: Reduced L-Glutathione and low-molecular-weight Hyaluronic Acid are sensitive to moisture and ambient degradation. By micronizing active powders and encapsulating them within a protective Virgin Olive Oil or Sunflower Lecithin lipid matrix, our softgels prevent oxidation, guaranteeing high bio-efficacy upon consumption.
Popular Custom Options: Vitamin E 400 IU (d-Alpha Tocopherol), Reduced Glutathione 500mg + Vitamin C, Hyaluronic Acid + Collagen Peptides.
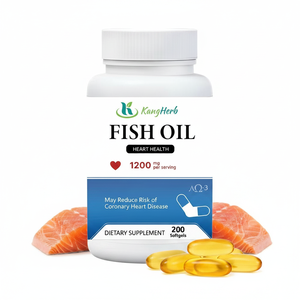
Omega-3 fatty acids are vulnerable to rancidity when exposed to heat, light, and oxygen. Our factory utilizes multi-stage molecular distillation to yield ultra-pure fish oil concentrates devoid of heavy metals, PCBs, and dioxins.
Technical Advantage: We offer customized EPA/DHA ratios—including Standard 18/12, High EPA 50/20 (for inflammatory & cardiovascular support), and High DHA 10/50 (for prenatal & cognitive health) in both Ethyl Ester (EE) and Triglyceride (TG) bio-identical lipid structures.
Popular Custom Options: 1000mg Deep Sea Fish Oil, High Potency Triple Strength Omega-3, Krill Oil + Astaxanthin Blends.
Cold-pressed natural seed oils and microalgae extracts require gentle processing parameters to preserve thermolabile bioactive components like Thymoquinone (TQ) and natural carotenoids.
Technical Advantage: Our Black Seed Oil (Nigella Sativa) softgels utilize 100% virgin cold-pressed oil, maintaining high TQ percentages without chemical solvent extraction. Astaxanthin softgels feature natural Haematococcus pluvialis extract encased in dark, light-blocking softgel shells to preserve antioxidant potency over a 36-month shelf life.
Popular Custom Options: Black Seed Oil 500mg/1000mg, Natural Astaxanthin 4mg/12mg, CoQ10 100mg + Black Seed Oil.
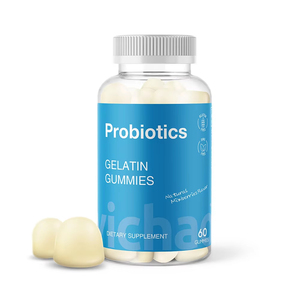
To accommodate brands expanding beyond traditional soft capsules, our plant manufactures advanced pectin-based functional gummies featuring heat-stable spore-forming probiotic strains.
Technical Advantage: Incorporating Bacillus coagulans into plant-based Citrus Pectin matrix guarantees high strain survival through high-temperature confectionery manufacturing and transit, delivering live colony forming units (CFU) directly to the gut.
Popular Custom Options: Sugar-Free Probiotic Pectin Gummies, Multivitamin Gummy Bears, Apple Cider Vinegar + Probiotics.
Every bulk softgel order follows an audited 10-step quality verification pipeline to guarantee batch-to-batch consistency and complete compliance.
All incoming oil carriers, active ingredients, and gelatin/tapioca granules are isolated in cleanroom quarantine pending full chemical verification.
Analytical chemists verify raw material raw purity and fingerprint identity using Fourier-Transform Infrared Spectroscopy (FTIR).
Oils and actives are homogenized in temperature-controlled stainless steel tanks under a vacuum and continuous nitrogen gas shield.
Gelatin or plant starch mass is cooked under vacuum to remove air bubbles, achieving optimal viscosity and moisture percentages.
High-precision injection pumps seal liquid fill material between two continuously rotating gelatin ribbons with laser-monitored seam thickness.
Freshly formed softgels pass through rotary tumble dryers under filtered dry airflow to rapidly set initial shell structural integrity.
Softgels are spread on food-grade trays in humidity-controlled cleanroom drying tunnels until target moisture level (6-8%) is reached.
High-speed optical camera sorting machinery scans 100% of capsules, automatically rejecting misshapen, discolored, or leaking softgels.
Finished batch samples are drawn for potency testing (HPLC), heavy metal testing (ICP-MS), and pathogen screening before QC sign-off.
Softgels are bottled, blistered, or drum-packed with desiccant packets, induction sealed, and loaded into export-ready freight containers.
Technical answers to common questions asked by brand owners, quality directors, and procurement managers.
Partner with an industry-leading contract manufacturer. Share your formulation requirements, custom product specifications, or target market goals with our engineering specialists today.
